china circuit breaker trip timing testing equipment solution - Bulk Supply and Specification Guide
How It Performs in Use
The complaint that repeats across reorders: timing drift after six months of daily substation work. Field crews report that the first trip test of the day reads 3.2 ms off from the last test of the previous shift, and the gap widens when the unit sits in a truck overnight at -10°C. Most quality disputes start with a consistency gap — the tester passes factory calibration at 23°C but delivers 0.5% measurement error once the internal temperature climbs 15°C above ambient during a 2000 A primary injection sequence.
A trip timing tester is judged on three numbers that appear in every tender: time measurement resolution (typically 1 µs), sampling rate per channel (minimum 10 kS/s, 100 kS/s for transient capture), and channel-to-channel skew (under 500 ns for differential protection schemes). The unit injects voltage or current into the breaker's control circuit, timestamps the contact change-of-state via high-speed digital inputs, and correlates that with the injected waveform. If the internal clock drifts more than 1 ppm/°C, the resulting COMTRADE file becomes useless for post-fault analysis — and that is the failure mode that triggers warranty returns.
Working Principle — What Actually Happens
The tester's FPGA generates a precisely timed trigger pulse. That pulse simultaneously starts the high-speed ADC acquisition across all analog and digital channels and drives the output amplifier stage. Contact sensors — either dry-contact sense inputs or optical isolators for high-voltage isolation — feed back to the same FPGA timestamp counter. The time delta between trigger and contact transition is the trip time. No PC software loop participates in the measurement; the PC only retrieves the timestamped dataset after the test completes. This architecture eliminates Windows jitter as a variable, but it means the FPGA clock oscillator's temperature coefficient becomes the single-point accuracy limiter.
Materials and Construction Trade-offs
| Subsystem | Standard Build | Upgraded Build | Impact on Field Life |
|---|---|---|---|
| Chassis | 1.5 mm powder-coated steel, IP40 | 2 mm stainless, IP54 with gasketed connectors | Corrosion at hinge points after 18 months coastal exposure |
| Digital inputs | Optocoupled, 250 V DC withstand | Fiber-optic isolated, 5 kV RMS withstand | Common-mode transients latch standard inputs; fiber survives |
| Output amplifiers | Linear, 30 V / 10 A per channel | Switching, 300 V / 20 A with active cooling | Linear runs hot; thermal shutdown interrupts long test sequences |
| Clock oscillator | TCXO, ±0.5 ppm initial, ±2 ppm/°C | OCXO, ±0.02 ppm initial, ±0.05 ppm/°C | TCXO drift exceeds IEC 61850-9-2 LE limits after 30 min warm-up |
Returns usually trace back to the same weak point: the BNC connectors on the analog input board. Standard nickel-plated brass lasts about 500 mating cycles before contact resistance rises above 50 mΩ, which adds measurable phase error at 10 kS/s. Gold-plated BNCs cost ¥18 more per channel but survive 5000 cycles. For a 16-channel unit, that is ¥288 per unit — a rounding error on a ¥120,000 FOB price, yet buyers consistently specify nickel to save the line item.
Specification Range and Customisation Limits
Every datasheet lists a range because no single configuration satisfies both the distribution utility doing annual maintenance on 11 kV vacuum breakers and the panel builder type-testing 400 A MCCBs to IEC 60947-2. The specification envelope is bounded by physics, not marketing:
- Analog channels: 4, 8, 12, or 16 — each adds a dedicated ADC and isolation barrier; 16 channels forces a 2U rack height
- Digital I/O: 8 to 64 optocoupled inputs, 4 to 32 relay outputs — ribbon-cable limited to 64 total pins per board
- Output voltage: 10 V, 30 V, 150 V, or 300 V DC — higher voltage requires creepage distances that reduce channel density
- Output current: 0.5 A, 2 A, 10 A, or 20 A per channel — 20 A needs forced-air cooling and a separate 3-phase inlet
- Timebase: TCXO (standard) or OCXO (option) — OCXO adds 45 minutes warm-up and 12 W continuous draw
- GPS/IRIG-B: factory-fit only; retrofitting requires replacing the rear-panel board and re-characterising the FPGA timestamp logic
Customisation stops at the FPGA firmware. The timestamping logic is burned into bitstream at final test; changing channel count or trigger logic requires a new bitstream build and full re-validation against IEC 61850-9-2 LE. We do not ship source HDL. Buyers who need protocol extensions (DNP3, IEC 60870-5-104) must specify them at order — the communication processor runs a separate RTOS image that is locked at shipment.
Option Comparison by Usage Level
Field Maintenance Tier
8 analog / 16 digital channels, TCXO timebase, 30 V / 2 A outputs, IP40 chassis, USB + Ethernet, COMTRADE export only.
- Weight: 6.2 kg with carry handle
- Operating temp: -10°C to 50°C
- Calibration interval: 12 months
- FOB range: ¥45,000–52,000
Chosen by: regional utilities with 2-person crews, contractor test vans. Fits in a Pelican 1650 case.
Type-Test Laboratory Tier
16 analog / 64 digital channels, OCXO timebase, 300 V / 20 A outputs, IP54 rackmount, dual Ethernet + IRIG-B + GPS, IEC 61850-9-2 LE streaming.
- Weight: 18 kg in 4U rack
- Operating temp: 0°C to 40°C (forced air)
- Calibration interval: 6 months (accredited lab)
- FOB range: ¥180,000–220,000
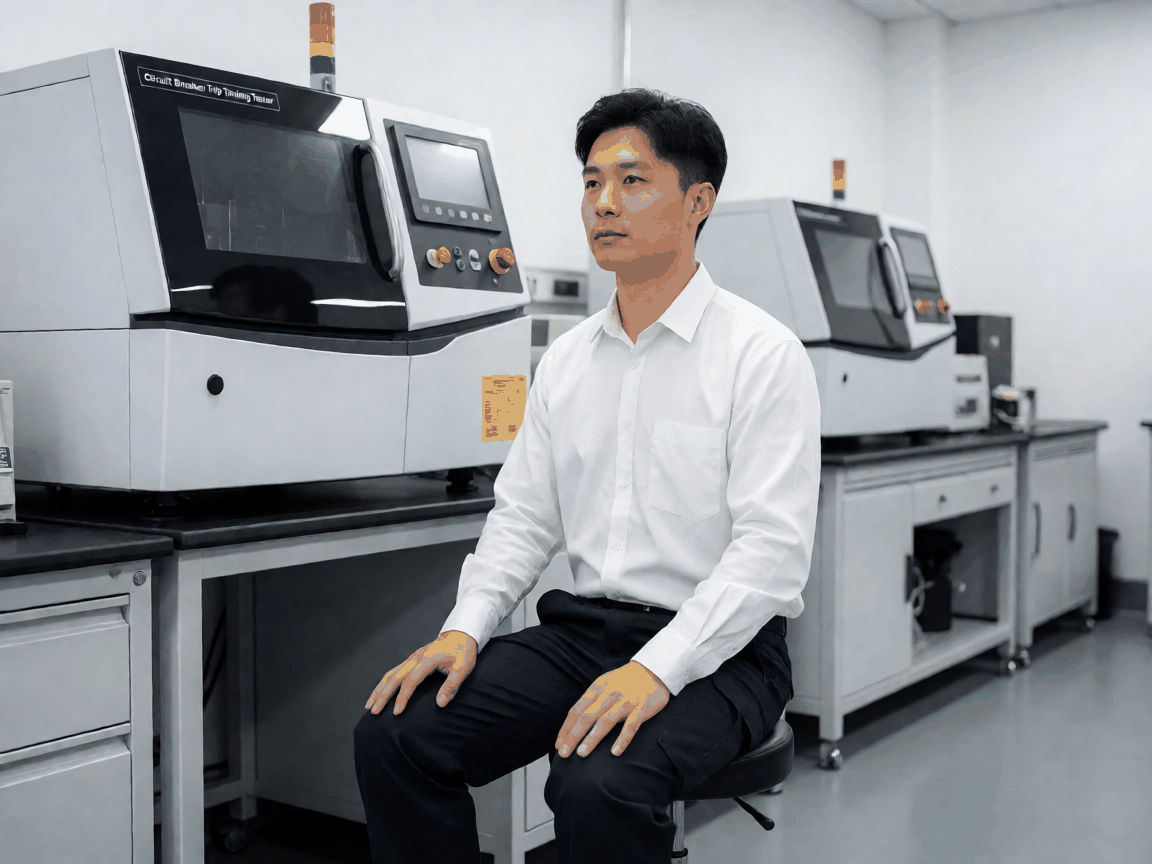
Chosen by: OEM breaker factories, accredited test labs, grid operator central labs. Requires 3-phase 380 V supply.
What Can Be Customised and What Cannot
| Customisable | Fixed at Design | Requires New Validation |
|---|---|---|
|
|
|
Artwork and branding review happens at the pre-production sample stage. We send a PDF proof of the overlay, the boot screen, and the default report header. The buyer signs off; any change after sign-off incurs a tooling delay of 10 working days and a ¥3,500 plate charge. Cable sets are kitted per order — standard 2 m leads unless specified. M12 connectors add ¥45 per channel for the connector itself plus ¥120 per cable for the overmoulded assembly.
How Consistency Is Held Across Batches
Batch Control Protocol
Each production lot (maximum 50 units) runs through a three-gate sequence. Gate 1: bare-board ICT and flying-probe on every PCB — open/short, component values, isolation resistance at 500 V DC. Gate 2: assembled unit functional test at 23°C ±2°C — all channels verified against a GPS-disciplined rubidium reference (Microchip 5071A) with 10 ns traceability. Gate 3: thermal soak at 40°C for 4 hours while running continuous 10 A injection on all channels; timestamp drift logged every 60 seconds. Units exceeding 0.8 ppm/°C drift are segregated for OCXO retrofit or scrap.
Component lot traceability is recorded in the MES: oscillator batch, ADC lot, FPGA date code, isolation barrier lot. A single lot change triggers a delta qualification — 5 units from the new lot run the full Gate 2/3 sequence before the lot is released for volume assembly. This is why lead time extends when a buyer specifies "same oscillator as last order" — we must confirm lot availability or run the delta qualification.
What Gets Checked Before Shipment
Final inspection is not a visual check. Every unit ships with a data packet that includes:
- Timebase accuracy certificate: measured at 23°C, 0°C, 40°C against the rubidium reference; ppm/°C slope reported
- Channel-to-channel skew report: all digital inputs triggered simultaneously via a calibrated pulse generator; max skew recorded
- Analog amplitude linearity: 10%, 50%, 100% of range, sine and DC; THD and DC offset at each point
- Isolation withstand: 2.5 kV RMS for 60 s between channel groups, channel-to-ground, and channel-to-communication ports
- EMC pre-scan: conducted emissions (150 kHz–30 MHz) and radiated emissions (30 MHz–1 GHz) per CISPR 11 Class A; no formal certificate unless buyer orders it
- Mechanical: connector retention (50 N pull), hinge cycle (100 open/close), handle pull (200 N)
The packet is a ZIP file on a USB stick taped inside the case lid. A printed summary sheet (one A4 page) sits on top for the receiving inspector who does not have a laptop at the loading dock. Buyers who need IEC 17025-accredited calibration must request it at order — it adds 5 working days and ¥8,500 per unit for the external lab slot.
Volume Planning and Lead Time
Standard configurations (Field Maintenance and Type-Test tiers) hold safety stock of 8–12 units in Shenzhen. These ship within 5 working days of PO receipt, provided artwork is pre-approved. Custom configurations start at 25 working days ARO for the first article — 10 days for PCB fabrication and assembly, 5 days for Gate 1/2 test, 5 days for thermal soak, 5 days for documentation and pack-out. Each additional 10 units adds 3 working days (panel build runs in batches of 10).
MOQ is 1 unit for standard tiers, 5 units for any custom channel count or voltage rating. Below 5 units, the per-unit test fixture setup cost (¥12,000) is not amortised and appears as a separate NRE line item. Forecast sharing helps: a rolling 6-month forecast with firm orders for month 1–2 lets us pre-position long-lead items (OCXO, 300 V output modules, FPGA). Without forecast, those items are ordered per PO and add 15 days.
Packaging: standard units ship in double-wall corrugated with custom-cut EPE foam (ISTA 2A qualified). Rackmount units ship in padded crates with shockwatch indicators. Palletisation is 4 units per Euro pallet for field tier, 1 unit per pallet for lab tier. Sea freight from Yantian adds 25–35 days to North Europe, 18–22 days to West Coast US. Air freight is 4–6 days door-to-door but costs 4.5× sea — only justified for launch-date-critical orders.
Next Steps — Artwork and Branding Review
If the specification envelope above matches your tender requirements, the next step is a configuration confirmation call. We will send a one-page configuration sheet listing every selectable option with the FOB impact of each. You mark the choices, attach your logo vector (AI or SVG, minimum 300 dpi at print size) and any regulatory mark artwork (CE, UKCA, RCM), and we return a PDF proof within 2 working days.
No tooling starts until you sign the proof. That sign-off is the gate that locks lead time.
Request configuration sheet and artwork proof template


