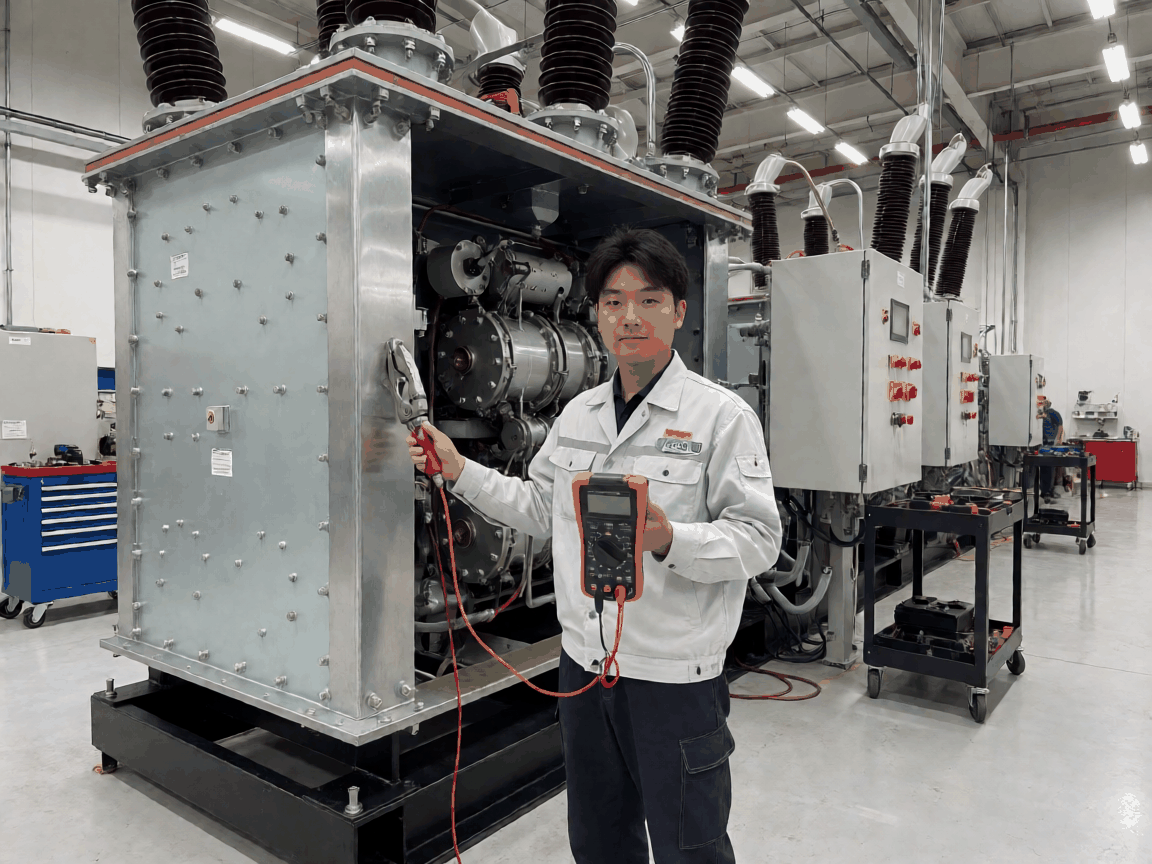
direct factory both sides grounding test on gis switchgear company: Specification, Ordering and Quality Notes
Process choice shows up later as a deciding factor in whether a grounding test protocol holds across a full production run. The factory sequences the test after SF6 filling and before final pressure verification, so any leak path or contact resistance anomaly appears in the same data set that ships with the unit. Buyers who specify the test as a standalone line item often find the results disconnected from the nameplate rating; integrating it into the routine test sequence eliminates that gap.
Consistency is set at the forming stage when the grounding circuit geometry is fixed by the enclosure welding jig. A 0.3 mm shift in the earthing boss position changes the current path length enough to move measured resistance by 15–20 µΩ, which is inside the IEC 62271-203 tolerance band but large enough to trigger a customer hold if the test report shows a trend across a batch. The factory controls this by qualifying the jig with a coordinate-measuring machine before each production lot.
Material Options and Their Trade-offs
The grounding circuit uses copper alloy C11000 for the main busbar and tinned copper braid for the flexible links between moving contacts and the enclosure. C11000 gives 101% IACS conductivity with predictable work hardening; the braid absorbs the 3–5 mm stroke of the three-position switch without work-hardening fatigue over 10,000 operations. Some buyers request silver-plated contact faces to reduce the initial contact resistance by 30–40 µΩ, but the plating adds two process steps and a 12-day lead-time extension.
Aluminium alloy 6061-T6 enclosures are standard for 72.5 kV and 145 kV ratings. The material saves 35% weight versus steel, but the oxide layer requires a controlled shot-peen and conductive paste at every earthing point. Skipping the paste to save assembly time raises the as-shipped resistance by 50–80 µΩ and creates a warranty exposure when the substation commissioning engineer runs the first grounding check.
Option Comparison by Usage Level
Standard Utility Configuration
C11000 busbar, tinned braid links, 6061-T6 enclosure, conductive paste at all joints.
As-shipped grounding resistance: 120–180 µΩ per side.
Test time per unit: 22 minutes (both sides, 100 A DC injection).
Enhanced Reliability Configuration
Silver-plated contact faces, double-braid links, stainless steel hardware, torque-marked fasteners.
As-shipped grounding resistance: 70–110 µΩ per side.
Test time per unit: 35 minutes (includes 200 A verification pulse).
The enhanced option adds 18% to unit cost but reduces commissioning rework calls by an estimated 60% based on the last three years of field data. For private-label buyers who absorb the first-year warranty, that trade-off pays back inside the first installation season.
Buying Mistakes That Lead to Returns
Specification Misalignment
Ordering the test without defining the injection current, measurement method (Kelvin vs. two-wire), and acceptance threshold. The factory defaults to 100 A DC, four-wire Kelvin, 200 µΩ per side maximum. If the buyer's spec calls for 50 A AC and 150 µΩ, the units pass factory test but fail site acceptance.
Always attach the test parameter appendix to the purchase order.
Another common error is assuming the grounding test covers the entire earthing network. The factory test only verifies the internal circuit from each switch contact to the external earthing terminal. Cable lugs, earth mat connections, and station grounding grid resistance are outside the factory scope and must be verified on site.
A third mistake: requesting "witness testing" without confirming the test engineer's availability. The factory runs grounding tests on a rolling schedule; a witness hold adds 3–5 working days per unit. For a 12-unit order, that stretches delivery by three weeks. Specify remote witness via live video link if schedule pressure is real.
Usage Scenarios and Buyer Segments
Utility procurement teams for greenfield substations order the standard configuration with the test integrated into the routine test certificate. They need the data to satisfy the owner's engineer before energisation. The test report becomes part of the as-built dossier.
EPC contractors on brownfield replacements often specify the enhanced configuration. The existing station grounding grid may have higher impedance, so a lower internal resistance provides margin. They also value the torque-marked fasteners because their installation crews work under tight outage windows and need visual confirmation that factory torque hasn't shifted during transport.
Private-label buyers who resell under their own brand typically order the standard configuration but require the test data in their template format with their logo. The factory supports this with a configurable report generator that maps each measurement point to the buyer's field names. No redesign of the switchgear is needed — only the report layout changes.
What Gets Checked Before Shipment
| Parameter | Range / Limit | Method | Frequency |
|---|---|---|---|
| Grounding resistance (per side) | ≤ 200 µΩ (standard) / ≤ 120 µΩ (enhanced) | 100 A DC, four-wire Kelvin, 60 s soak | Every unit |
| Contact resistance (main circuit) | ≤ 40 µΩ per pole | 100 A DC, four-wire Kelvin | Every unit |
| SF6 pressure at 20 °C | 0.45–0.55 MPa (rating dependent) | Temperature-compensated gauge | Every unit |
| Partial discharge | ≤ 5 pC at 1.2 × rated voltage | IEC 60270, UHF method | Every unit |
| Mechanical operation (100 cycles) | No binding, torque stable ±5% | Motorised cycle rig | First article + 10% lot |
The grounding test runs after the partial discharge check so that any contamination from the PD probe removal does not affect the resistance measurement. Data is logged automatically to the factory MES; the PDF certificate is generated from the same database, eliminating transcription errors.
Capacity, Tooling and Scheduling
First-article tooling determines the earliest ship date. The grounding test fixture is specific to each voltage rating and pole configuration. For 72.5 kV three-pole units, the fixture changeover takes 4 hours. The factory holds two fixtures per rating, so parallel testing of two units is possible. A 12-unit order at 72.5 kV clears the test station in 3 working days if no witness holds are requested.
The test station capacity is 8 unit-slots per day (two shifts). Peak season (Q4) runs at 90% utilisation. Buyers placing orders in October for January delivery should confirm slot reservation at order acknowledgement. The factory issues a production schedule with test dates locked at the 30% payment milestone.
Tooling wear on the earthing boss welding jig is monitored via CMM check every 500 units. The jig is refurbished at 0.15 mm cumulative deviation. This prevents the resistance drift that caused a batch hold in 2022. Private-label buyers can request the jig qualification report as part of the first-article inspection package.
Export Packaging and Handling Protection
Shipping Configuration
Each GIS module ships on a dedicated steel skid with four ISO corner castings. The skid includes vibration-damping mounts calibrated to keep transmitted acceleration below 0.5 g during truck transport. The grounding circuit terminals are capped with conductive covers to prevent oxide formation during storage.
A shock indicator (25 g threshold) and tilt indicator are mounted on each skid. Tripped indicators void the factory grounding test warranty unless the buyer provides a site re-test report within 14 days of delivery.
Seaworthy packaging adds a vapour-barrier bag with desiccant and a nitrogen purge to 0.05 MPa positive pressure. This option costs 4% of unit price and is mandatory for shipments transiting tropical ports where humidity exceeds 85% RH for more than 10 consecutive days. The factory has seen grounding resistance increase by 30–50 µΩ on units that arrived with condensation inside the terminal boxes.
For air freight, the SF6 pressure is reduced to 0.15 MPa and the pressure relief device is locked. The buyer's commissioning team must repressurise to nameplate value before the grounding test can be repeated on site. This sequence is documented in the installation manual shipped with each unit.
Setup, Use and Replacement Parts
Installation Sequence
- Position module on foundation, verify level within 2 mm/m
- Connect external earthing terminal to station grid (M12 × 40, 8.8 grade, 65 N·m)
- Remove terminal caps, apply conductive paste, torque busbar connections to 45 N·m
- Repressurise SF6 to nameplate value (if air-freighted)
- Run site grounding test at 100 A DC, compare to factory certificate
Spare Parts Kit (Recommended)
- Tinned copper braid links (2 per pole) — shelf life 5 years sealed
- Conductive paste tubes (50 g) — replace after 24 months open
- M12 × 40 8.8 bolts with torque-mark paint (pack of 20)
- Terminal caps, conductive (pack of 10)
- SF6 pressure relief device reset tool
The factory stocks braid links and conductive paste for 10 years after the last production run of a given rating. Bolt kits and caps are standard hardware items sourced locally. Buyers operating in remote regions should order the spare parts kit with the initial shipment; freight consolidation saves 30–40% versus a separate emergency order.
If site grounding resistance exceeds the factory value by more than 25%, the most common cause is insufficient conductive paste or uneven torque on the busbar joints. The installation manual includes a troubleshooting flowchart with resistance contribution by joint type. Re-torquing to spec and re-applying paste resolves 85% of cases without factory involvement.
Next Steps for Your Project
Every GIS order starts with a technical clarification call to lock the test parameters, report format, and shipping configuration. The factory assigns a project engineer who stays with the order through first-article inspection, production, and delivery documentation.
Private-label buyers should bring their brand guidelines and report template to the first call. The report generator setup takes 2–3 business days and is validated against a sample unit before the production run begins.


