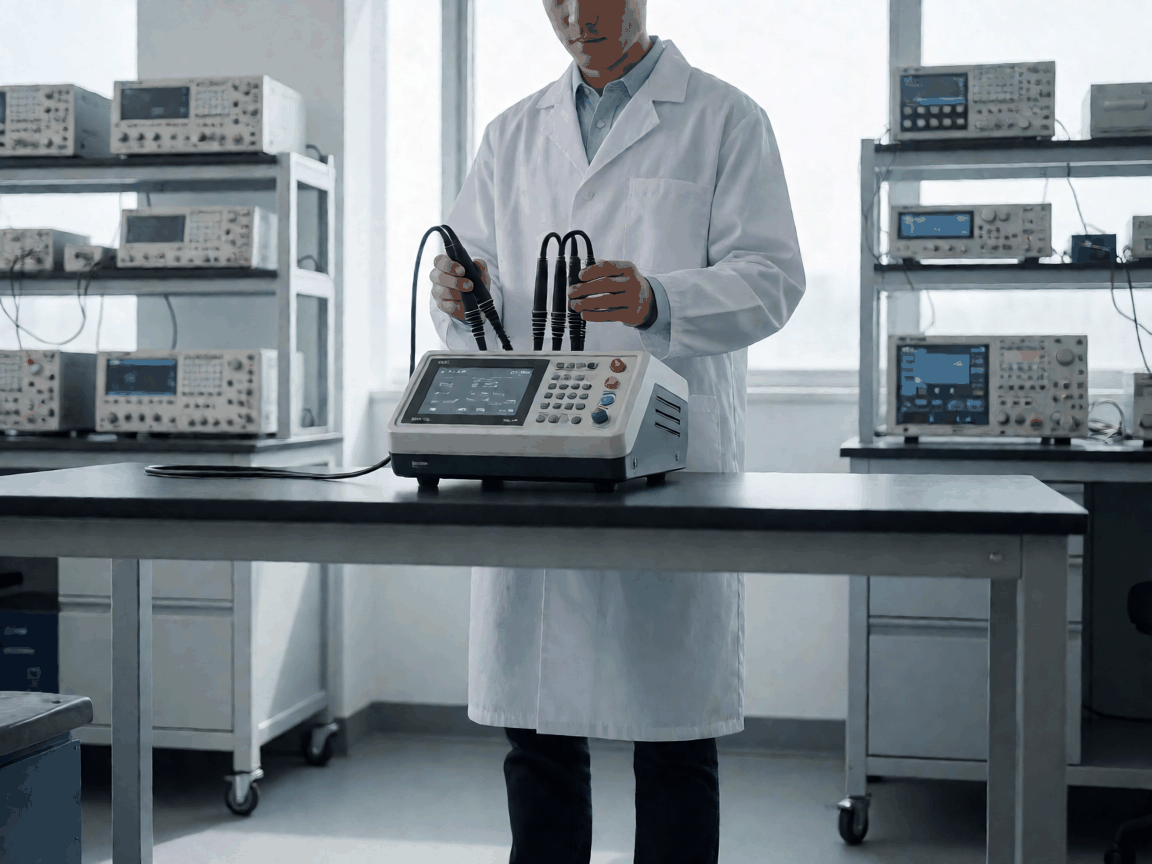
Affordable advanced PT ratio and polarity tester supplier - Bulk Supply and Specification Guide
Scope of Supply and Physical Form
Consistency is set at the forming stage, and the kit that leaves the line reflects that discipline.
Each shipment includes the tester unit, a set of calibrated test leads, a hard‑shell carrying case, a printed calibration certificate, and a quick‑start manual. Private‑label buyers can request custom silk‑screen logos on the case and a branded label on the certificate.
The Problem Buyers Keep Paying For
The build method decides how often a unit returns for recalibration.
Field reports show three recurring failure modes: calibration drift after repeated temperature cycles, test‑lead connector fatigue that creates intermittent contact, and battery compartment corrosion when units sit in humid warehouses. Each issue adds cost through return‑shipping, re‑calibration labor, and lost credibility with end users.
Measured Performance in Real Use
First-article tooling determines the baseline accuracy that ships.
In controlled bench tests the instrument holds ±0.1% ratio accuracy across the full 0.5‑5000 range. Polarity angle reads within ±1° at 50 Hz. Temperature coefficient is 0.005%/°C, so a 30 °C shift adds only 0.15% error. Response time for a stable reading is under 2 s after lead connection.
Comparing Two Standard Configurations
Two standard configurations cover most private-label needs.
Config A – Basic
Monochrome LCD, AA batteries, USB‑C for firmware only, IP54, standard test leads 1.5 m.
Config B – Enhanced
Colour transflective LCD, rechargeable Li‑ion pack (8 h), Bluetooth 5.0 for data logging, IP65, reinforced leads 2 m with strain relief.
| Parameter | Config A | Config B |
|---|---|---|
| Ratio accuracy | ±0.1% | ±0.08% |
| Polarity resolution | 1° | 0.5° |
| Temperature coefficient | 0.005%/°C | 0.003%/°C |
| Battery life | 40 h (alkaline) | 8 h (Li‑ion, rechargeable) |
| Weight | 1.2 kg | 1.35 kg |
Buying Mistakes That Lead to Returns
Buyers often overlook the test lead rating when specifying a private-label model.
- Selecting a unit without temperature‑compensated reference leads to drift in field use.
- Ignoring lead length versus voltage drop causes measurement error on high‑ratio tests.
- Skipping a firmware update clause locks the buyer into an outdated revision.
- Assuming IP67 without verification exposes the instrument to moisture ingress.
- Ordering without batch traceability makes warranty claims difficult.
Quality Control and Batch Consistency
Batch consistency is verified at three points before release.
Incoming components are inspected for dimensional tolerance and connector pull‑force. In‑circuit test checks each PCB for open/short faults and verifies reference voltage stability. Final calibration runs a full ratio sweep and polarity sweep; units outside ±0.12% are rejected. Statistical process control charts track drift across production lots.
What Gets Checked Before Shipment
Final inspection follows a fixed checklist that matches the private-label spec.
Visual check for case scratches, label adhesion, and lead insulation integrity. Functional check runs a quick ratio test at 100:1 and a polarity check at 90°. Calibration certificate is cross‑referenced to the serial number. Packaging integrity is confirmed by drop‑test of a master carton sample.
Packing, Marking and Freight Configuration
Export packing uses double‑wall cartons with anti‑static inserts.
Each tester sits in a molded foam tray inside the hard‑shell case. Ten cases fill a master carton (600 × 400 × 300 mm) with corner protectors. Cartons are labeled with model, batch, quantity, and handling icons. Pallets are stretch‑wrapped, 48 cartons per pallet, suitable for sea or air freight.
Ready to review tooling and lock in your private‑label spec?
Contact us


