Specifying wholesale current transformer polarity ratio analyzer factory for Wholesale and OEM Orders
What the Design Has to Balance
| Parameter | Typical Range | Impact on Total Cost |
|---|---|---|
| Ratio Accuracy Class | 0.1% – 0.5% (IEC 61869) | Tighter class reduces recalibration frequency; each 0.1% step adds 15–20% unit cost |
| Primary Current Injection | 100 A – 2000 A | Higher range covers more CT sizes but increases transformer weight and shipping class |
| Polarity Detection Method | Phase-shift vs. DC kick | Phase-shift works on loaded CTs; DC kick needs isolation — choose by field workflow |
| Enclosure Rating | IP54 – IP67 | IP67 adds 1.2 kg and 18% cost; required for substation yard work |
| Battery Runtime | 6 – 14 hours continuous | Hot-swappable packs cost more upfront but eliminate downtime on multi-day commissioning |
Total cost of ownership shifts once returns are counted. A 0.5% class analyzer priced 30% below the 0.2% model looks attractive until the utility rejects commissioning reports and demands re-test with traceable gear. The 0.2% unit pays for its premium after two avoided revisits. Weight matters too — a 9 kg box with IP54 rating gets carried up transformer platforms; a 14 kg IP67 unit stays in the truck and the crew rents a competitor's kit. Design the spec around the harshest site the buyer visits monthly, not the lab bench.
Materials and Construction Trade-offs
Aluminum Chassis + Polycarbonate Overmold
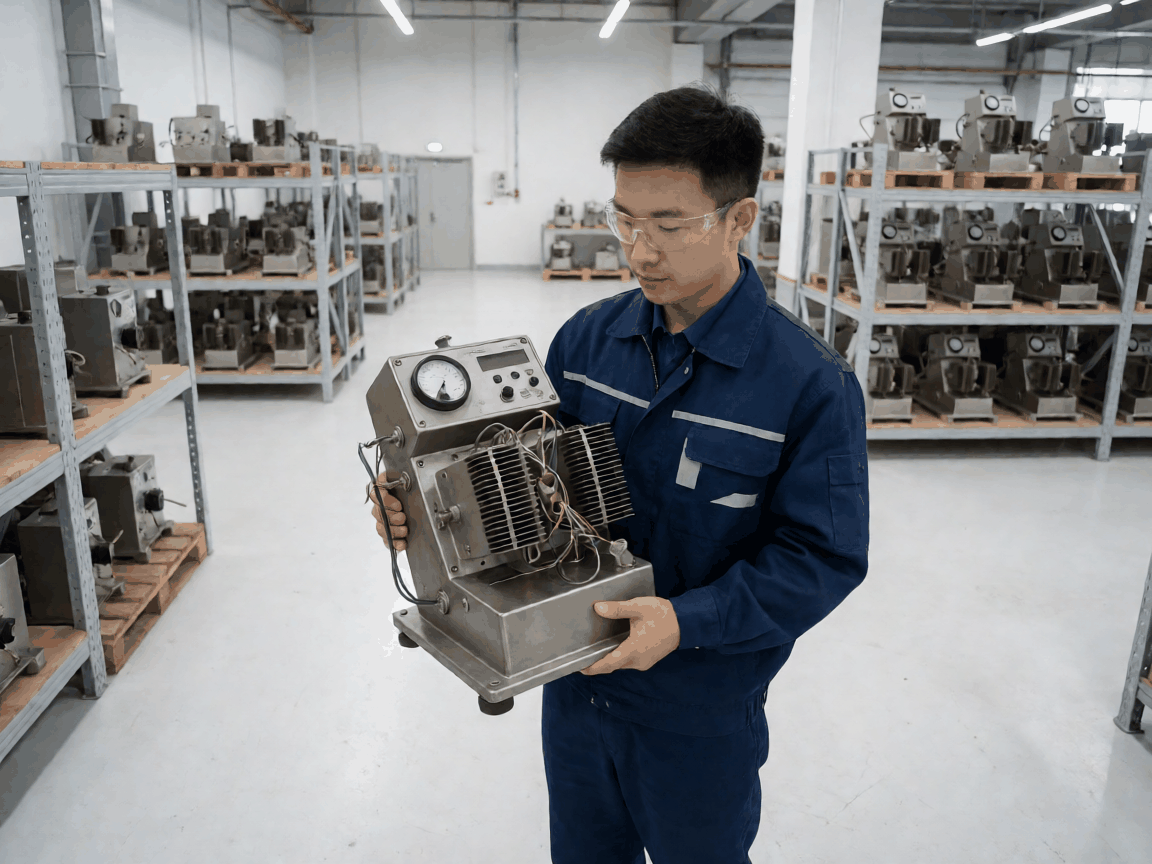
CNC-machined 6061-T6 frame dissipates heat from the 2 kVA injection transformer. Overmolded corners survive 1 m drops onto concrete — the failure mode that kills plastic-enclosed rivals. Adds 800 g versus full polymer shell.
Best for: utility crews doing daily substation rounds where the analyzer rides in a bucket truck.
Full Polymer (GFR-PA66) with Internal Ribs
30% glass-filled nylon cuts 1.5 kg and meets IP65. Ribs prevent flex-induced PCB cracking — the #1 warranty claim on lighter units. Not rated for direct arc-flash exposure; keep behind barriers.
Best for: panel shops and OEM test benches where the unit stays on a cart.
The injection transformer winding insulation defines service life. Class H (180°C) enamel on the primary withstands 15-minute continuous injection at 2000 A without derating. Class F (155°C) forces a 50% duty cycle — crews learn to pause, doubling test time. Spec Class H for rental fleets; Class F passes for in-house QC where tests run 30 seconds per CT.
Buying Mistakes That Lead to Returns
Replacement rate, not unit price, drives the real expense. Three patterns cause 80% of returns:
- Selecting secondary-injection-only models for field crews who must verify polarity on energized CTs — phase-shift method needs primary injection capability.
- Skipping the IP67 upgrade for coastal substations; salt ingress corrodes the BNC connectors within six months, corrupting ratio readings by 0.3–0.8%.
- Ordering fixed-test-lead sets instead of modular Kelvin clips. Fixed leads fracture at the strain relief after 200 insertions; modular clips swap in 30 seconds and cost 12% more per set.
Cheaper stock options fail at the worst point in the season — spring commissioning when crews are maxed out. A $400 saving on leads generates a $4,000 revisit charge when the utility inspector rejects the test sheet.
Usage Scenarios and Buyer Segments
Utility transmission teams run 50–80 CT tests per week across 115 kV–500 kV yards. They need IP67, hot-swappable batteries, and phase-shift polarity on live circuits. Panel builders test 5–10 CTs per batch in controlled shops; they prioritize 0.1% ratio accuracy, USB-C data export, and bench-mount brackets. Rental houses buy fleets of 20+ units — they specify Class H insulation, modular leads, and firmware-locked calibration intervals to prevent unauthorized adjustments. Each segment demands a different accessory kit: utility gets high-voltage probe extenders and rain covers; panel builders get short Kelvin leads and DIN-rail mount adapters; rental gets rugged cases with foam cutouts for spare batteries and probe sets.
Quality Control and Batch Consistency
Calibration Traceability Protocol
Every unit ships with a factory calibration certificate referencing a primary standard traceable to NIST or NMISA. The certificate lists ratio error at 10%, 50%, 100%, and 120% of rated primary current, plus phase displacement at each point. Batch consistency is verified by testing the first, middle, and last unit of each production run against the same reference CT — maximum spread 0.03% ratio error, 0.02° phase. Units outside tolerance are re-calibrated or scrapped; no statistical sampling substitutes for 100% verification on this product line.
Firmware version and calibration date are stored in non-volatile memory and displayed at boot. Buyers can audit compliance without opening the case.
Volume Planning and Lead Time
Standard configurations (0.2% class, IP54, 1000 A primary, modular leads) hold 4–6 week lead time at 10–50 unit volumes. Custom firmware branding, special probe sets, or IP67 upgrades add 2 weeks. Orders above 100 units trigger a dedicated production cell — lead time drops to 3 weeks but requires 50% deposit and frozen spec 30 days before build start. Rental fleet buyers typically stage deliveries: 20 units month one, 20 month two, balancing cash flow against calibration expiry alignment. We hold safety stock of Class H transformers and polycarbonate overmolds to absorb 20% surges without extending published lead times.
Questions Buyers Ask Before Ordering
Can the analyzer test CTs with residual magnetism? Yes — the DC demagnetization routine runs automatically before each ratio test, clearing remanence up to 80% of knee-point voltage. Adds 15 seconds per test.
What happens if the battery dies mid-sequence? Test data auto-saves to internal flash every 5 seconds. Hot-swap the pack; the analyzer resumes at the next tap without data loss. Non-hot-swap models lose the current test record.
Is the calibration certificate accepted by IEEE C57.13 and IEC 61869 compliance audits? Yes, provided the buying organization's quality system accepts factory traceability. For accredited-lab requirements, we arrange third-party ISO 17025 calibration before shipment — adds 5 business days and $320/unit.
Can we private-label the enclosure and startup screen? Minimum 30 units. Laser-etched logo on the overmold, custom boot logo, and branded calibration certificate template. No firmware changes — liability stays with our calibration lab.
What freight packaging survives air freight to remote sites? Each unit ships in a Peli-type case with custom foam (IP67 rated). Palletized shipments use edge-protected double-wall cartons with humidity indicators. We document drop-test results (1.2 m, 3 axes) for insurer approval.
Next Steps
Send your test volume, site conditions, and required accuracy class to our applications team. We'll return a configured BOM with accessory kit options, lead time, and a calibration schedule that matches your audit cycle. Artwork files for private labeling go to the same address — vector format, Pantone references, and minimum 300 dpi at final size.


